Molding, decoration, and assembly on one floor.
Senwell runs injection and bi-injection molding, spray coating and vacuum metallization, automated silk screening and hot stamping, and cleanroom assembly. Components are molded, decorated, assembled, and packed out without leaving the site.
In-House Capabilities
Everything below is installed at Hung Yen. Molding, decoration, coating, and assembly all run on the same site, so a component doesn't leave the building between processes.
| Hung Yen, Vietnam | |
|---|---|
| Floor area | 100,000 sq ft |
| Injection machines | 20 |
| Tonnage range | 160–290T |
| Molding processes | Injection, bi-injection |
| Decoration | Silk screening, hot stamping |
| Coating | 2 spray lines, 2 vacuum metallization chambers |
| Automation | Automated assembly, hot stamping, silk screening |
| Tooling | Tool maintenance shop on site |
| Assembly | Automated and manual lines, cleanroom environment |
| Headcount | 150+ |
| Certifications | ISO certified · LEED Gold facility |
| Nearest port | Haiphong — 1.5 hrs |
Figures current as of July 2026 · Vietnam capacity expanding
Injection Molding
Twenty presses from 160 to 290 tonnes, with take-out robots on the line. Bi-injection runs two materials or two colors in a single cycle — for soft-touch surfaces, multi-tone caps, and parts where a bonded second shot beats a secondary assembly step.
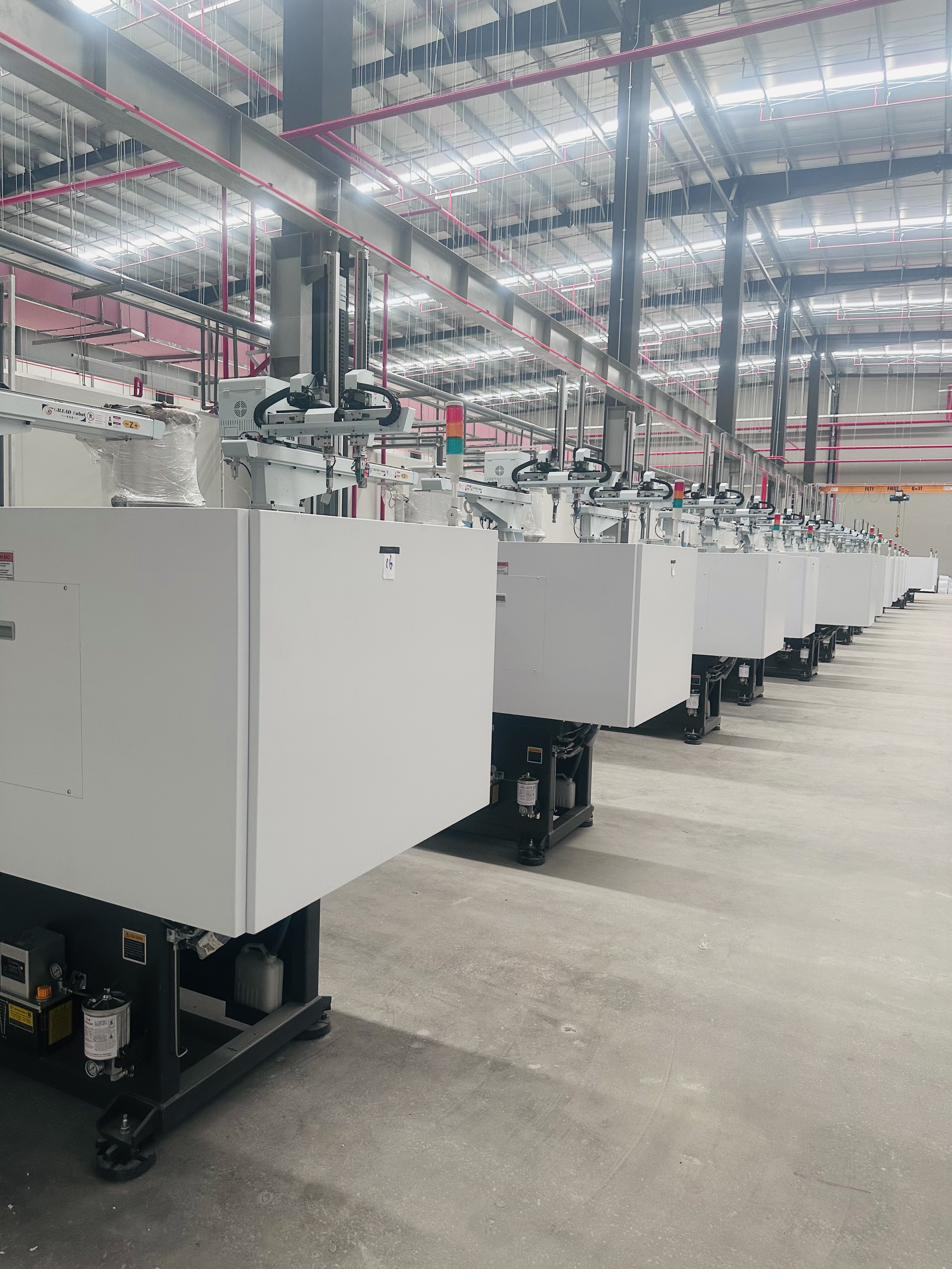 Fig. 01 — Molding Hall
Decoration
Silk screening and hot stamping both run automated, which is what holds registration across a long run rather than drifting part by part.
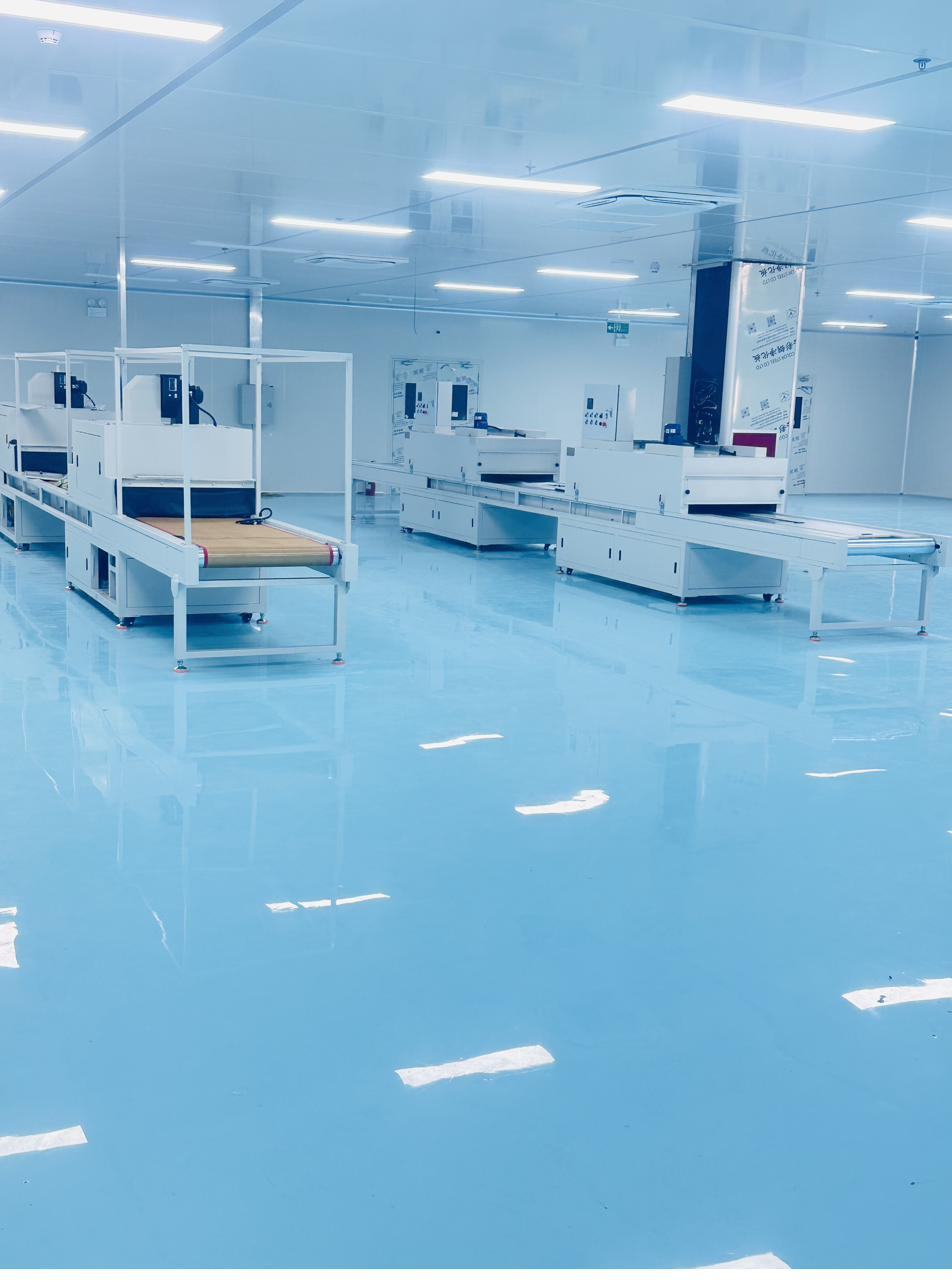 Fig. 02 — Decoration Line
Coating & Metallization
Two spray lines and two vacuum metallization chambers. Keeping metallization on site matters for beauty work: the chrome and metallic finishes that sell a cap are also the ones most likely to be rejected, and having the chamber on the floor means a failed batch is diagnosed in hours rather than shipped back to a vendor.
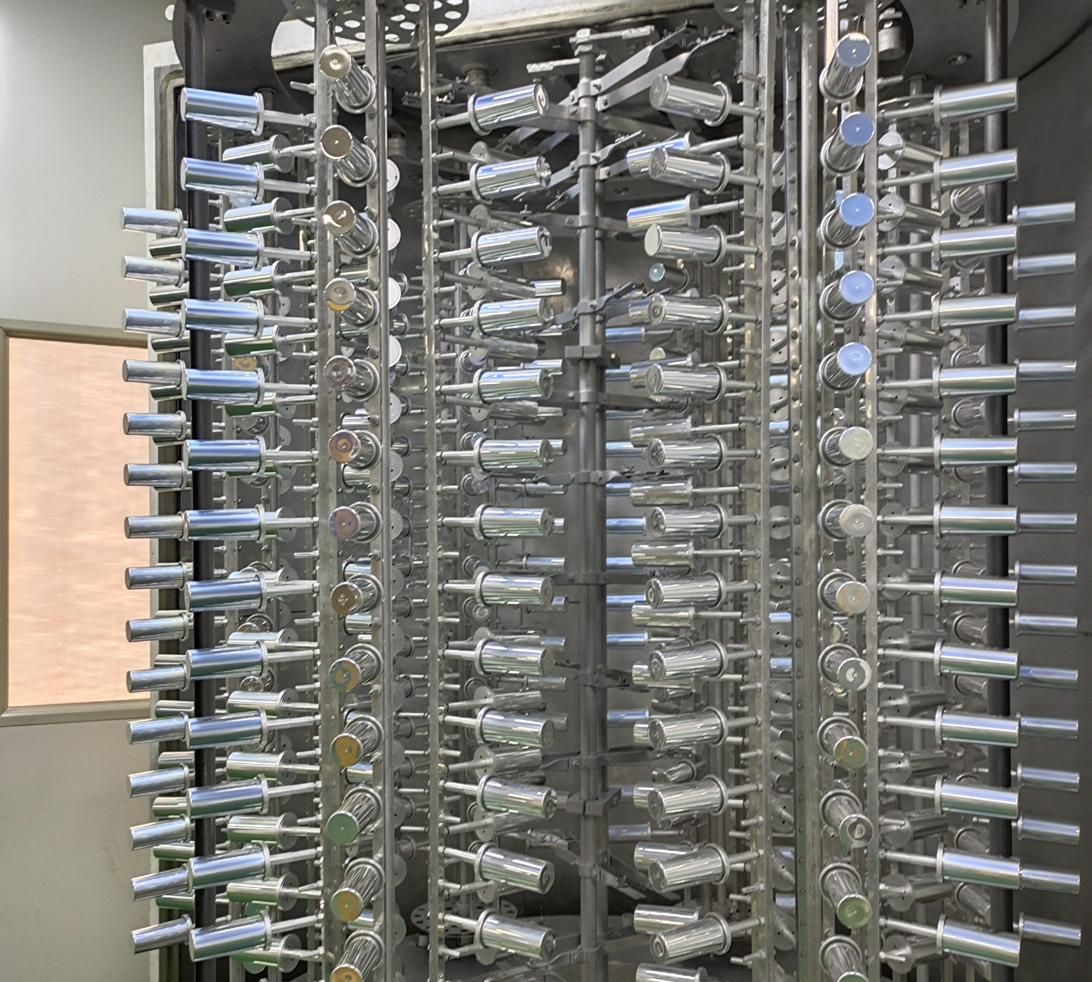 Fig. 03 — Coating Line
Assembly
Automated and manual assembly lines in a controlled cleanroom, with QC before pack-out. Components leave the site assembled and cartoned, ready to go straight to a filler.
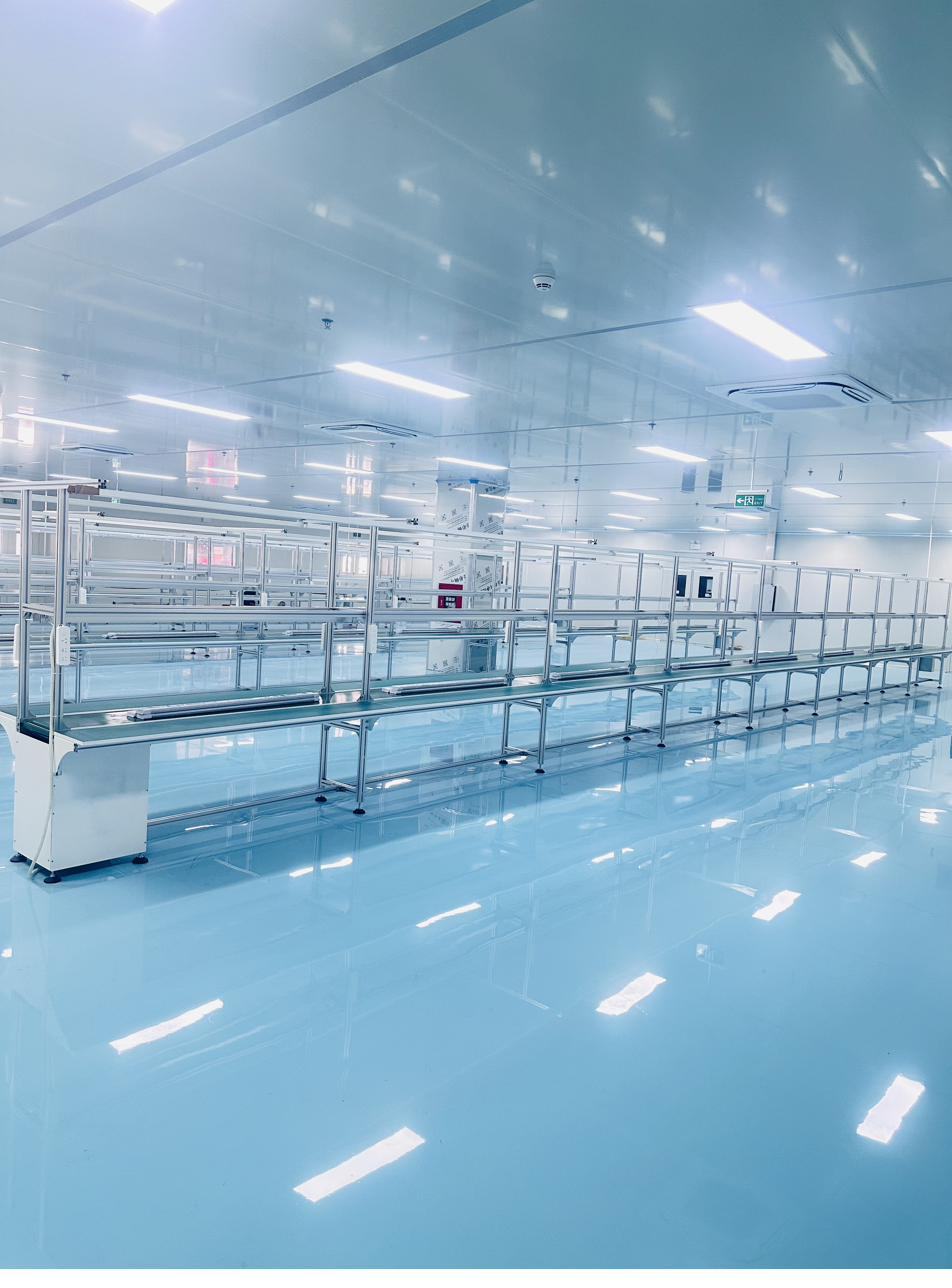 Fig. 04 — Cleanroom Assembly
From Kickoff to Delivered Carton
Every program runs through the same three phases, with one project manager from kickoff to delivered carton. Engineering questions get answered by the people who will run the tool.
Development
- Kickoff and program scoping
- Stock or custom packaging proposals
- Engineering and tooling development
- Testing and commercialization
Production
- Pre-production sign-off
- Purchasing and supply chain
- Molding, decoration, assembly
- Quality control before pack-out
Logistics
- Export from Haiphong or Noi Bai
- Fill and secondary assembly support
- Documentation and compliance
- Final delivery
Scope your program with our engineers.
Send drawings, an existing mold, or a reference sample with your target cost and volumes. We'll tell you what's realistic to build here, and what it will cost.